Chemical Reactor Manufacturers, Suppliers & Exporters in Hosur
Primesol & Ergo System is a prominent Chemical Reactor Manufacturers in Hosur, Suppliers and Exporters in Hosur. We offer engineered process equipment solutions for industrial applications and have more than decade industrial experience. Our company ISO 9001:2015 verified and designed for controlled mixing, heating, cooling and processing of different materials across chemical and manufacturing applications.
We supply robust, corrosion-proof chemical reactors to processing units operating in SIPCOT Phase I, SIPCOT Phase II, and Mathigiri. Designed for batch synthesis, polymerization, and mixing, our chemical reactors ensure maximum yield and continuous operation. We offer dedicated sourcing and engineering backup for chemical manufacturing hubs throughout Hosur.
Our Reactor Manufacturing solutions can be customized according to material characteristics, process conditions, working volume, operating temperature, pressure requirements and equipment layout. Our systems are suitable for industries including chemicals, pharmaceuticals, agrochemicals, food processing, specialty chemicals and other process industries.
Chemical Reactor Manufacturers, Suppliers and Exporters in Hosur
As experienced Industrial Reactor Vessels Suppliers in Hosur, our robust reactor systems cater to diverse industries, supporting controlled chemical reactions, mixing and processing of liquids, powders and other compatible materials across Hosur and international destinations. Backed by engineering expertise, we provide reliable reactor solutions designed according to process requirements, material compatibility, temperature conditions and pressure requirements.
What is a Chemical Reactor?
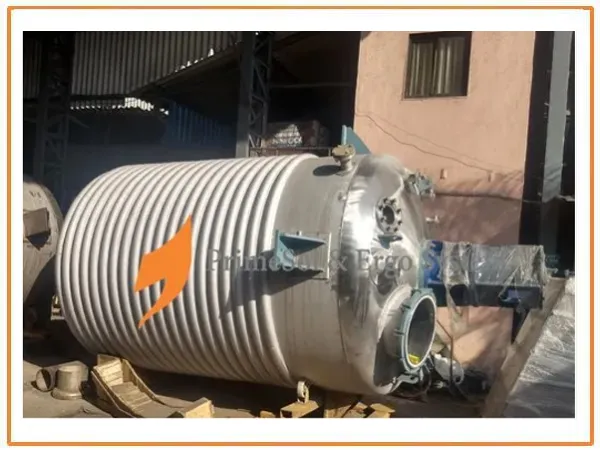
Chemical Reactor is a process vessel used to carry out controlled chemical reactions under defined operating conditions. It provides a suitable environment for mixing, heating, cooling and processing different materials according to the requirements of a particular chemical process. A Reactor Vessel generally consists of a vessel body, agitator or mixing arrangement, inlet and outlet connections and suitable heating or cooling provisions.
Purpose of Chemical Reactor
The main purpose of a Chemical Reactor is to provide controlled conditions for carrying out chemical reactions and industrial processing operations.
Provide a controlled environment for chemical reactions.
Mix and process liquids, powders and other suitable materials.
Maintain required reaction temperature through heating or cooling.
Support controlled processing under atmospheric or pressurized conditions.
How Does Our Chemical Reactor Work?
Material Charging- Raw materials, chemicals, solvents or other suitable ingredients are introduced into the Reactor Vessel through the designated inlet or charging arrangement.
Material Mixing- An agitator or suitable mixing mechanism rotates inside the vessel to provide controlled mixing according to the material and process requirements.
Heating or Cooling- The required process temperature can be maintained using a jacket, limpet coil, internal coil or other suitable heat-transfer arrangement.
Controlled Reaction- The materials remain inside the reactor for the required processing or reaction time under specified temperature, pressure and mixing conditions.
Product Discharge- After completion of the required process, the processed material is discharged through the designated outlet and transferred to the next stage of production.
What are Different Types of Chemical Reactors We Provide?
As experienced Chemical Reactor Manufacturers in Serving Across Hosur, we provide different reactor configurations according to process requirements, material characteristics, operating temperature, pressure and application conditions.
Jacketed Reactor- Jacketed Reactors feature an external jacket around the reactor vessel through which a heating or cooling medium can be circulated. This arrangement helps control the temperature of the material inside the vessel during chemical processing and reaction operations.
Limpeted Reactor- Limpeted Reactors use a limpet coil arrangement around the vessel to provide heating or cooling to the process material. The heat-transfer arrangement can be selected according to the required temperature range, vessel size, process conditions and thermal requirements.
MS Reactor- MS Reactors use Mild Steel construction and can provide a practical solution for suitable general industrial processing applications. They can be designed according to required working volume, material characteristics, operating temperature, pressure and plant requirements.
Chemical Reactor- Chemical Reactors are designed for carrying out controlled chemical reactions, mixing and processing operations in industrial environments. The vessel configuration can be selected according to reaction conditions, material compatibility, required volume, temperature and pressure requirements.
Stainless Steel Reactor- Stainless Steel Reactors are manufactured using stainless steel construction for applications requiring suitable corrosion resistance, hygienic surfaces and compatibility with process materials. SS 304 and SS 316 can be selected according to the chemical properties and operating conditions of the application.
Technical Specification of Chemical Reactor
As Chemical Reactor Suppliers in Hosur, we provide reactor systems with specifications selected according to process, reaction and material handling requirements.
Specification
Typical / Available Range
Reactor Type
Chemical Reactor / SS Reactor / Jacketed Reactor / Limpet Reactor / MS Reactor
Working Capacity
100–20,000 Litres
Material of Construction
MS / SS 304 / SS 316
Operating Pressure
Atmospheric to 10 Bar
Operating Temperature
Up to 250°C
Agitator Type
Paddle / Anchor / Propeller / Turbine
Agitator Speed
20–150 RPM
Motor Power
1–50 HP
Heating Arrangement
Jacket / Limpet Coil / Internal Coil
Cooling Arrangement
Jacket / Limpet Coil / Cooling Medium
Vessel Orientation
Vertical / Customized
Vessel Design
Cylindrical / Customized
Surface Finish
Industrial / Smooth / Polished as Required
Drive Type
Geared Motor / Direct Drive
Inlet / Outlet
Customized According to Process
Insulation
Available as Required
Importance of Chemical Reactor Systems
Controlled Chemical Processing- Chemical reactors provide controlled conditions for carrying out chemical reactions according to specified process requirements.
Temperature Control- Jacketed and limpet arrangements can help maintain the required process temperature during heating and cooling operations.
Consistent Mixing- High Pressure & Flow Reactors Suitable agitator arrangements support controlled mixing of compatible liquids, powders and other process materials.
Process Integration- Reactor systems can be connected with pumps, pipelines, storage tanks, condensers, filters and other process equipment.
What are the Advantages of Our Chemical Reactor?
As Industrial Reactor Vessels Exporters in Hosur / Hosur, Primesol & Ergo System develops reactor solutions with features selected according to specific process and manufacturing requirements.
Multiple Reactor Configurations- We provide Reactor Manufacturing, Reactor Vessel, Jacketed Reactors, Limpet Reactors and MS Reactors according to application requirements.
Application-Specific Construction- The material of construction can be selected according to chemical compatibility, process conditions, operating temperature and pressure requirements.
Controlled Heating and Cooling- Industrial Reactor Vessels and limpet coil arrangements can be incorporated to support controlled temperature management during processing.
Customized Agitation Systems- Different agitator configurations can be selected according to viscosity, material characteristics, mixing requirements and process conditions.
Suitable for Different Process Conditions- Our Reactor Vessels can be designed for suitable atmospheric or pressurized processing applications based on project requirements.
Where Our Chemical Reactor is Applicable?
As Chemical Reactor Manufacturers in Hosur, our reactor solutions can be used across different manufacturing and process industries.
Chemical Industry- Chemical Reactors can be used for controlled reactions, mixing, heating and processing of compatible chemicals. The reactor construction and process arrangement can be selected according to chemical properties and operating conditions.
Pharmaceutical Industry- Stainless Steel Reactors can support suitable pharmaceutical processing applications where controlled mixing, temperature management and hygienic construction are required. Reactor design depends on process, material and cleanliness requirements.
Agrochemical Industry- Chemical reactors can assist in processing suitable agrochemical materials and formulations. Material of construction, agitation and temperature control arrangements can be selected according to chemical compatibility and process requirements.
Specialty Chemical Industry- Reactor Vessels can be used for various specialty chemical processing operations requiring controlled reaction conditions. Reactor configuration can be customized according to material properties, reaction temperature and pressure.
Resin and Polymer Applications- Industrial Reactor Vessels can be used for compatible resin, polymer and formulation processes requiring controlled mixing and temperature management. Agitator and heating arrangements can be selected according to viscosity and process conditions.
Chemical Reactor Performance Evaluation
The performance of a Chemical Reactor should be evaluated according to the actual process requirements.
Testing Conditions
Material type and chemical characteristics.
Required working and total volume.
Operating pressure requirements.
Material viscosity and density.
Key Evaluation Parameters
Reaction consistency.
Mixing performance.
Temperature control.
Pressure handling capability.
Agitator performance.
Chemical Reactor Maintenance and Services in Serving Across Hosur
Regular inspection and timely maintenance are important for maintaining reliable Chemical Reactor performance and safe operation.
Maintenance activities may include:
Checking reactor vessel body and connections.
Inspecting agitator shaft and impeller condition.
Checking motor and gearbox condition.
Inspecting jacket or limpet coil connections.
Checking inlet and outlet nozzles.
Inspecting seals and gaskets.
Monitoring unusual noise or vibration.
How Does Chemical Reactor Cost Determine
Important factors include:
Material of construction.
Operating temperature.
Operating pressure.
Agitator type and speed.
Jacket or limpet coil arrangement.
Reactor type.
Working and total capacity.
Why Choose Primesol & Ergo System?
ISO 9001:2015 Certified- We are an ISO 9001:2015 Certified company, highlighting our focus on quality management and consistent manufacturing practices.
10+ Years of Experience- Primesol & Ergo System is reported as established in 2015, giving the company 10+ years of industry experience. Its experience covers industrial equipment, process engineering and manufacturing solutions.
24×7 Service Commitment- The website states that the company is ready to provide services 24×7, supporting its positioning around responsive customer service.
Affordable Cost & On-Time Delivery- The company's website highlights affordable cost, on-time delivery and quick response as key customer-facing strengths.
Primesol & Ergo System is a trusted Chemical Reactor Manufacturers in Hosur, Suppliers and Exporters in Hosur. We also provide High Pressure & Flow Reactors and customized Industrial Reactor Vessels according to specific application requirements. We offer precision-engineered reactor solutions for diverse industrial processing applications. Our range includes Chemical Reactors, Stainless Steel Reactors, Jacketed Reactors, Limpet Reactors and MS Reactors, tailored according to material characteristics, working capacity, temperature, pressure, mixing requirements and process conditions. Contact us today to discuss your project requirements or request a custom quote for Chemical Reactors in Hosur
FAQs
A chemical reactor enables controlled chemical reactions under specified operating conditions to produce the required products or intermediates.
Common types include batch reactors, continuous stirred tank reactors, plug flow reactors, and jacketed reactors. Selection depends on the reaction and production process.
Chemical manufacturing, specialty chemicals, pharmaceuticals, agrochemicals, and other process industries use chemical reactors for suitable production applications.
Yes, reactors can be engineered for specified pressure and temperature conditions when the design, materials, fabrication, testing, and safety systems meet the applicable requirements.
Evaluate process engineering capabilities, material compatibility, pressure-vessel design expertise, fabrication quality, inspection and testing practices, and compliance with applicable standards.
Hi there! 👋
Fill out the form below to start a conversation with us on WhatsApp.
Hi there! 👋
Fill out the form below to start a conversation with us on WhatsApp.